How to Interpret Height-Gauge Calibration Results: Error Patterns, Surface Plate Effects & ISO 13225 Review
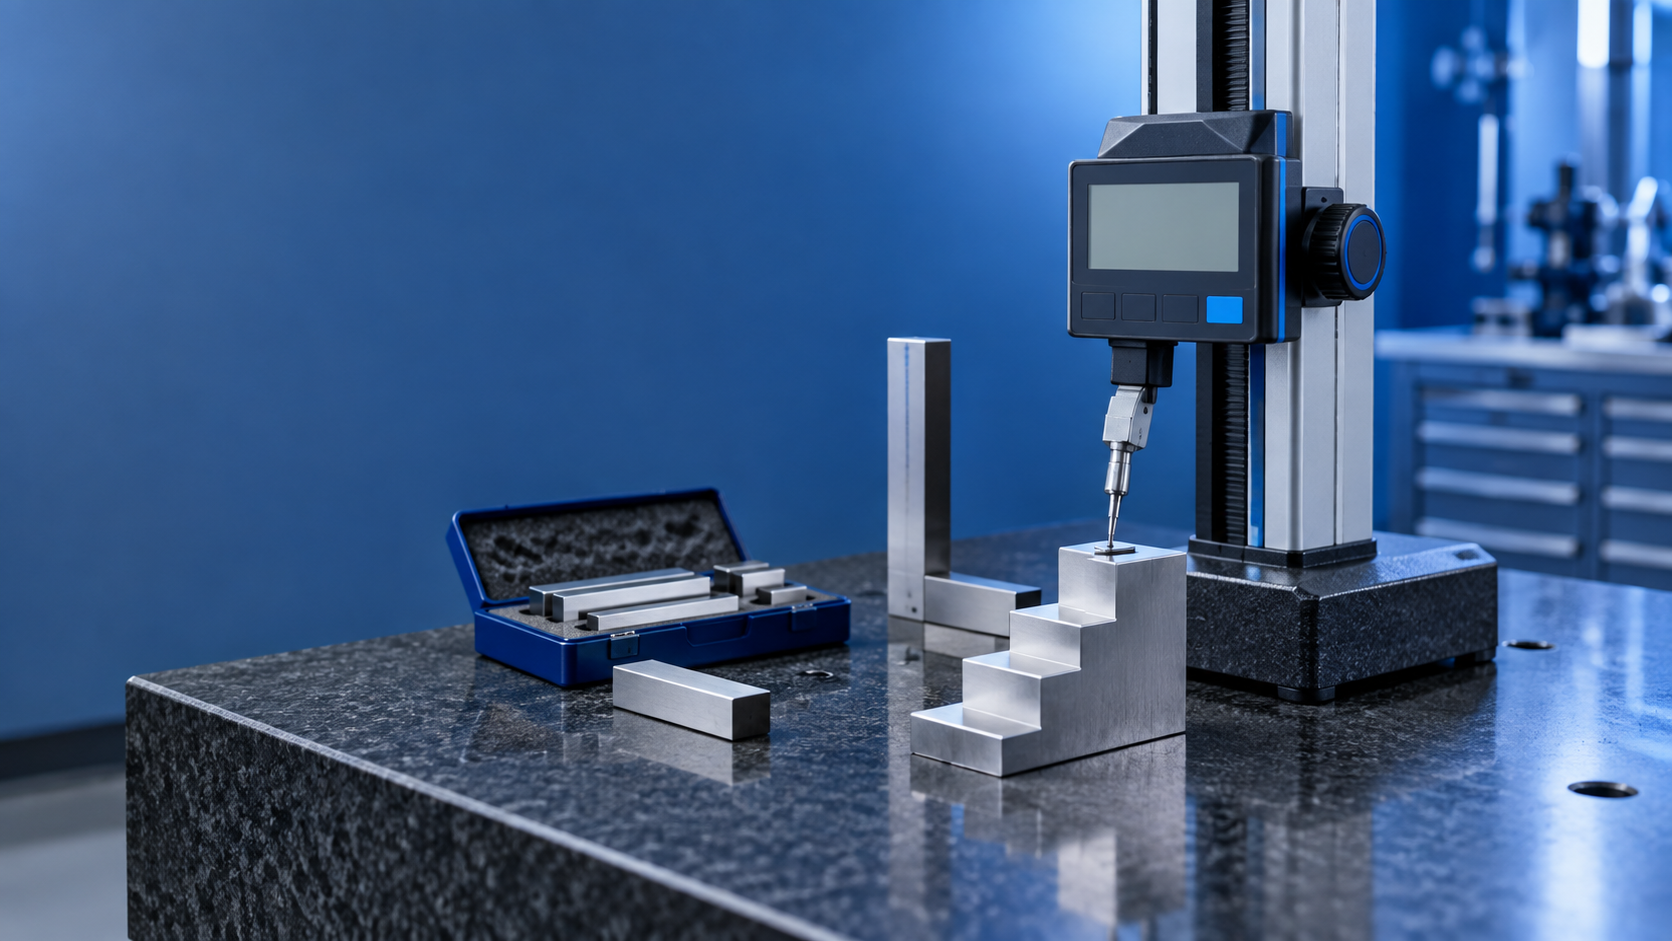
Never judge a height gauge by its digital display resolution or a single passing test point. Unlike an outside micrometer that closes around a workpiece between two self-contained anvils, a height gauge measures every coordinate relative to an external reference datum. That means the granite surface plate, base pad flatness, vertical column squareness, slider carriage play, probe overhang, and direction of travel all combine to shape the indicated number.
Reading a height-gauge calibration certificate effectively requires looking past a binary “PASS” stamp. By analyzing how errors behave across the vertical column—and comparing the laboratory’s calibration setup against your shopfloor inspection bench—you can spot mechanical wear, column tilt, and probe deflection before they corrupt product acceptance decisions.
1. What a Height-Gauge Certificate Actually Evaluates (ISO 13225)
ISO 13225:2012 defines the design and metrological characteristics for analog, dial, digital, and motorized 1D/2D height gauges operating on a surface plate. When an accredited laboratory calibrates a height gauge against long gauge blocks, a step gauge, or a laser interferometer, the reported values reflect the combined behavior of seven physical variables:
- Base Reference Plane Flatness: Micro-burrs, rust pitting, or dirt trapped beneath the hardened cast-iron/steel base pad tilt the entire vertical column.
- Surface Plate Local Flatness: Any hollow trough or local curvature in the granite surface plate between the height gauge base and the reference standard shifts the relative datum height.
- Column Perpendicularity & Straightness: Forward or lateral bow along the vertical beam introduces progressive cosine and Abbe offset errors as the slider climbs higher.
- Slider Carriage & Gib Clearance: Loose gibs or worn guide rollers allow the carriage to pitch up or down when the probe contacts a surface.
- Probing Element Geometry: Carbide scribers, spherical ruby touch probes, and lever dial indicators each introduce distinct cantilever lengths and mechanical bending deflections.
- Contact Force & Approach Direction: Approaching a feature from below versus above introduces mechanical backlash and bidirectional hysteresis.
- Differential Thermal Expansion: As documented in NIST Monograph 180 (The Gauge Block Handbook), temperature deviations from 20°C cause steel gauge blocks and height-gauge scale encoders to expand at different rates unless thermally soaked.
2. Decoding Error Patterns Across the Vertical Span
At each calibrated height position, the fundamental indication error is defined algebraically as:
Note: Always verify the certificate’s sign convention first. If a report tabulates “Correction (C = R − I),” the algebraic signs will be reversed.
Examining the trajectory of E from the bottom of the column to the top reveals the underlying mechanical health of the instrument:
| Observed Error Trajectory | Mechanical / Metrological Mechanism to Investigate |
|---|---|
| Constant Offset Across All Heights (e.g., +0.025 mm at 50, 200, 400, and 600 mm) |
Improper zero/origin datum setting on the granite plate, dirt under the reference block base, uncompensated scriber tip wear, or probe ball offset miscalculation. |
| Error Grows Linearly With Height (e.g., +0.005 mm at 100 mm → +0.035 mm at 600 mm) |
Column out-of-squareness relative to the base pad, progressive Abbe tilt across a long scriber overhang, linear encoder scale pitch error, or uncompensated thermal expansion mismatch. |
| Isolated Spike at One or Two Points (e.g., 0.000 mm everywhere except +0.040 mm at 300 mm) |
Localized nick on the rack gear teeth, chipped capacitive/optical encoder strip, dried grease clot on the column guideways, or burred step-gauge master facet. |
| Stable Lower Span, Divergent Upper Span (e.g., within ±0.005 mm below 250 mm; drifts above 400 mm) |
Upper column bending, worn upper guide ways (or undamaged upper ways contrasted with heavily worn lower ways), or granite surface plate edge drop-off during testing. |
| Bidirectional Divergence (Up vs. Down) (Ascending reading differs from descending reading) |
Excessive slider carriage gib play, rack-and-pinion backlash, flexing scriber clamp, or inaccurate probe ball diameter compensation calibration. |
3. Direction of Travel, Hysteresis & Bidirectional Probing
When inspecting simple step heights above the surface plate, the scriber or probe contacts every feature from above (descending travel). However, when measuring groove widths, slot thicknesses, or bore diameters and centerlines, the probe contacts the bottom surface while moving downward and the top surface while moving upward.
4. Probe, Scriber & Cantilever Overhang Effects
Because the height-gauge scale is housed inside the vertical column while the contact point extends outward on a horizontal arm, every height gauge violates Abbe’s collinearity principle. The resulting Abbe error is directly proportional to the horizontal overhang length (Larm) multiplied by the angular pitch of the slider carriage (θ):
Doubling the length of a custom extension scriber or indicator arm doubles the vertical measurement error caused by carriage pitch.
| Probing Accessory Condition | Metrological Impact on Production Measurements |
|---|---|
| Loose Scriber Clamp or Adapter | Shifts the reference zero mid-inspection; ruins repeatability across successive touches. |
| Worn Flat on Carbide Scriber Tip | Alters the effective contact line when scribing or zeroing against the granite datum vs. rounded part edges. |
| Long Custom Extension Arm | Amplifies elastic cantilever bending and carriage pitch error beyond what a standard short-probe calibration captured. |
| Inconsistent Operator Hand Force | On vernier and digital hand-wheel height gauges without a constant-force clutch, heavy hand pressure lifts the front edge of the base pad off the granite by microns. |
5. Repeatability vs. Indication Error: Worked 0–600 mm Case Study
Never confuse Repeatability (R) with Indication Error (E). A height gauge can repeat within 0.002 mm across five touches and still read 0.045 mm off true height due to column tilt. Conversely, an instrument with a near-zero average error is unusable if loose carriage gibs cause consecutive readings to scatter by ±0.030 mm.
Worked Case Study: Evaluating a 0–600 mm Digital Height Gauge
Suppose your quality department receives the following As-Found calibration table for a 0–600 mm digital height gauge (allowable MPE limit: ±0.030 mm, expanded uncertainty U = 0.006 mm at k = 2). On your shop floor, this gauge is used exclusively to inspect machined housings between 50 mm and 220 mm:
| Nominal Height (R) | Mean Indication (I) | Indication Error (E) | Repeatability (s) | MPE Limit | Zone Assessment |
|---|---|---|---|---|---|
| 50.000 mm | 50.003 mm | +0.003 mm | 0.001 mm | ±0.030 mm | Conforming (Active Zone) |
| 150.000 mm | 150.006 mm | +0.006 mm | 0.002 mm | ±0.030 mm | Conforming (Active Zone) |
| 250.000 mm | 250.009 mm | +0.009 mm | 0.002 mm | ±0.030 mm | Conforming (Upper Bound) |
| 450.000 mm | 450.028 mm | +0.028 mm | 0.003 mm | ±0.030 mm | Borderline (Unc. Overlaps) |
| 600.000 mm | 600.042 mm | +0.042 mm | 0.003 mm | ±0.030 mm | Out-of-Tolerance (OOT) |
- Past Product Risk (Reverse Traceability): Because all shopfloor production parts measured between 50 mm and 220 mm, where the actual error was ≤ +0.009 mm, previously shipped housings were not compromised by the 600 mm failure.
- Equipment Release Options: Before returning the gauge to the floor, quality engineering must either (1) send the column for mechanical squareness realignment and recalibration, or (2) formally issue a Restricted/Limited Calibration Release (0–250 mm Only) with a physical mechanical stop or prominent yellow restriction label if permitted by plant quality procedures.
6. Height-Gauge Diagnostic Matrix
Use this quick-reference troubleshooting table when reviewing anomalous calibration certificates or shopfloor inspection disputes:
| Observed Symptom | What to Check First | Dangerous Assumption to Avoid |
|---|---|---|
| Constant offset across all heights | Granite zeroing spot, base burr, probe clamping tightness, and certificate sign convention. | Assuming the encoder scale is accurate simply because repeatability is tight. |
| Error grows steadily with height | Column perpendicularity to base, long probe overhang, and thermal stabilization time. | Assuming a single 100 mm check block verifies the 500 mm upper range. |
| Upward vs. downward readings differ | Slider gib play, constant-force clutch slip, and probe-ball diameter compensation value. | Assuming approach direction does not matter on digital encoders. |
| Erratic repeatability at one height | Localized column dent, rack debris, loose indicator clamp, or oil film on granite. | Averaging 5 erratic readings to force a passing number without fixing the looseness. |
| Calibrated gauge disagrees on shop floor | Shopfloor granite surface plate wear (Grade 1/2 trough), part clamping distortion, and operator hand pressure. | Blaming the height gauge when the shopfloor surface plate is worn out of flat. |
| Zero shifts after returning to plate | Encoder strip slippage, low battery voltage, or dirty base pads picking up metal swarf. | Assuming an initial morning zero remains valid for an entire 8-hour shift. |
7. 11-Point Return-to-Service Release Checklist
Complete this verification gate before signing off on a height-gauge calibration certificate and releasing the instrument to inspection teams:
✓ Height-Gauge Certificate Release Sign-Off
- 1. Asset & Probe Identity: Serial number, model, range, resolution, and attached probe/scriber match the physical unit.
- 2. Span Coverage: Calibrated test points bracket the entire vertical working height used in production.
- 3. Error Trajectory Audited: Full error curve reviewed for progressive slope, local spikes, or hysteresis—not just the summary PASS stamp.
- 4. Sign Convention Confirmed: Verified whether table reports Indication Error (I − R) or Correction (R − I).
- 5. Repeatability & Hysteresis Checked: Repeatability (RMPE) and bidirectional probing values meet process requirements.
- 6. Shopfloor Surface Plate Verified: Confirmed that the granite surface plate where the height gauge operates holds an active, in-tolerance flatness calibration (ISO 8512-2 / IS 7327).
- 7. Uncertainty & Decision Rule Applied: Expanded uncertainty (U at k = 2) accounted for at tolerance boundaries per ILAC-G8.
- 8. As-Found vs. As-Left Preserved: Both pre-adjustment and post-adjustment datasets archived in the gauge history folder.
- 9. OOT Impact Evaluated: If As-Found failed in the active working zone, a formal Out-of-Tolerance product containment review was executed.
- 10. Range or Accessory Restrictions Tagged: Any limited height range or dedicated probe configuration is clearly labeled on the column.
- 11. Formal Release Logged: Reviewer signature, release date, and next calibration due date updated in the calibration management system.
Frequently Asked Questions
A height gauge measures height relative to the surface plate beneath its base. In the calibration laboratory, it is tested on a pristine Grade 0 reference granite plate. If the shopfloor granite plate has a worn hollow in the center where parts are placed while the height gauge base rests on the unworn outer rim, every measurement will be systematically offset by the depth of that granite wear trough.
ISO 13225:2012 defines the design features and metrological characteristics (such as Error of Indication E_MPE and Repeatability R_MPE) for height gauges. A laboratory's accredited calibration procedure specifies the operational step-by-step method, master artifacts (step gauge, long gauge blocks, or laser interferometer), environmental bounds, and GUM uncertainty calculation used to quantify those characteristics.
Ideally, calibrate the height gauge in the exact configuration used for inspection. Using a sensitive lever indicator or electronic touch probe during calibration eliminates human contact-force variation to isolate scale accuracy, but if operators use a long, heavy carbide scriber on the floor, you must also verify scriber base-zero alignment and overhang deflection.
Yes, provided your quality management system permits 'Limited/Restricted Calibration' dispositions and the failure is caused by gradual upper-column geometry rather than damaged electronics or loose carriage gibs. You must document the engineering review, verify that no production parts exceed the approved lower range, and affix a clear physical restriction label onto the instrument.
Need Accredited Height-Gauge, Step-Gauge or Surface Plate Calibration?
Connect directly with Multitek Technologies engineers for NABL ISO/IEC 17025 accredited calibration of digital height gauges, 2D height masters, granite surface plates, and dimensional standards.
Request Technical Quotation / DemoExplore Related Metrology & Calibration Resources
- Dimensional Calibration Planning: Practical Engineering Guide
- Caliper Calibration Error Interpretation & Abbe Offsets
- As-Found and As-Left Measurement Impact Review
- Out-of-Tolerance (OOT) Calibration Containment & Impact Analysis
- Decision Rules, Guard Bands & Conformity Assessment
- Calibration in Engineering Metrology: VIM Clause 2.39 & GUM Budgets
- NABL ISO/IEC 17025 Accredited Calibration Services
- Contact & Service Quotation Request